Deburring machines / BB, HB, HBB
Slag and Dross
Removal Machines
Thick plate comes off a high-power laser, plasma or oxy-fuel table with slag welded to the bottom edge. Chipping and grinding it off by hand is slow, dirty and different every time. Lasvio slag removal machines break it off and clean the surface in one pass, so plate goes straight to weld prep or coating.
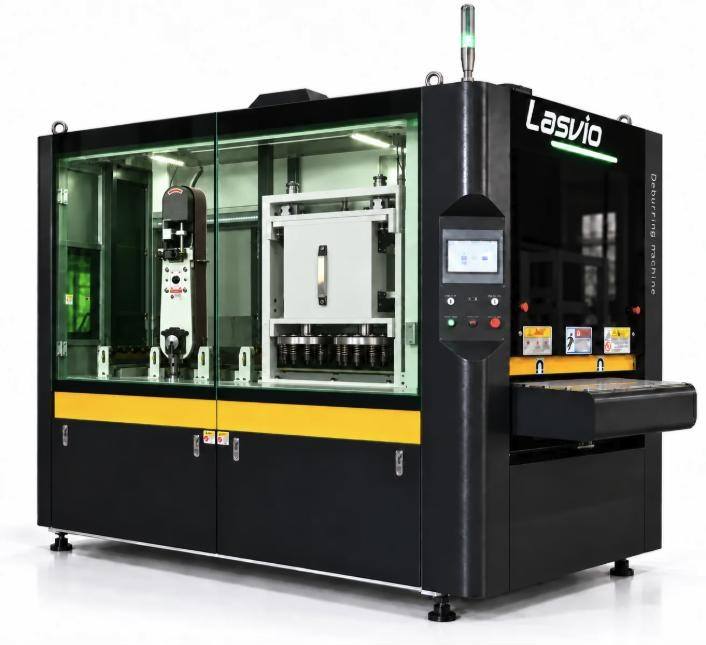
What heavy slag costs you
BB, HB or HBB: which one
The choice comes down to how firmly the slag is attached and how clean the part needs to be afterwards.
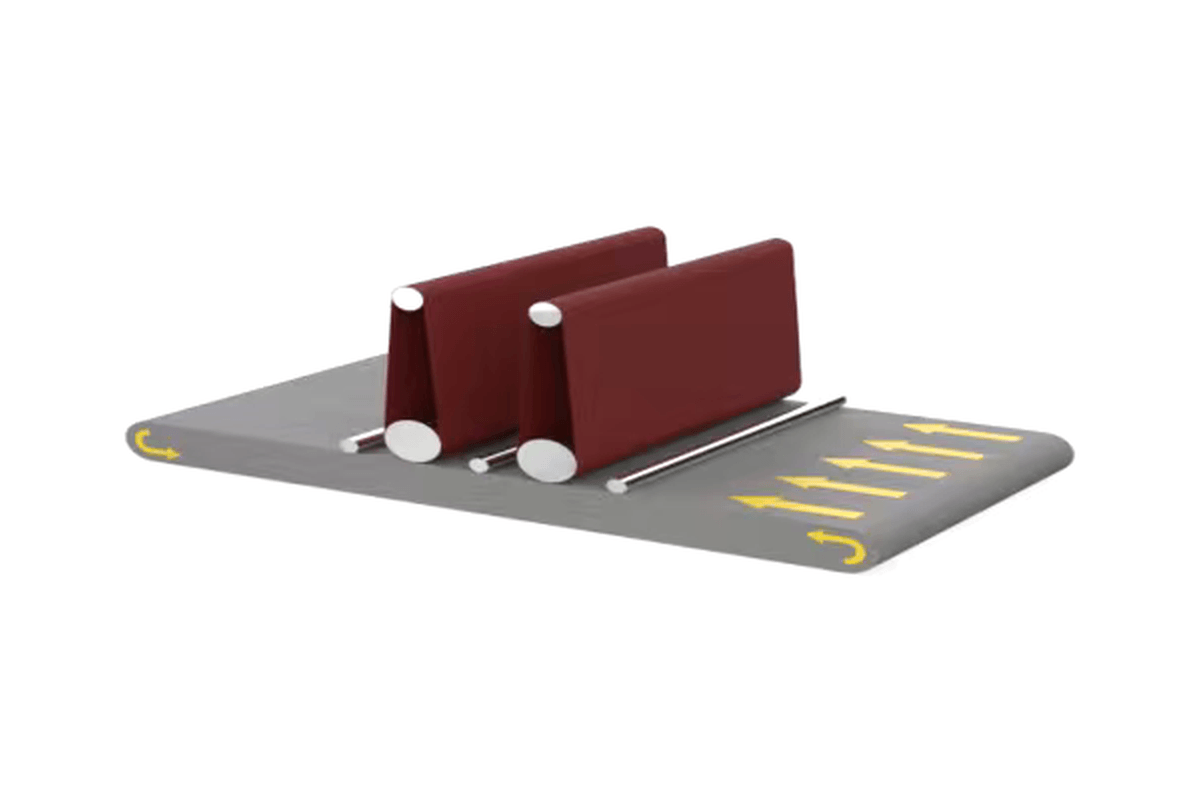
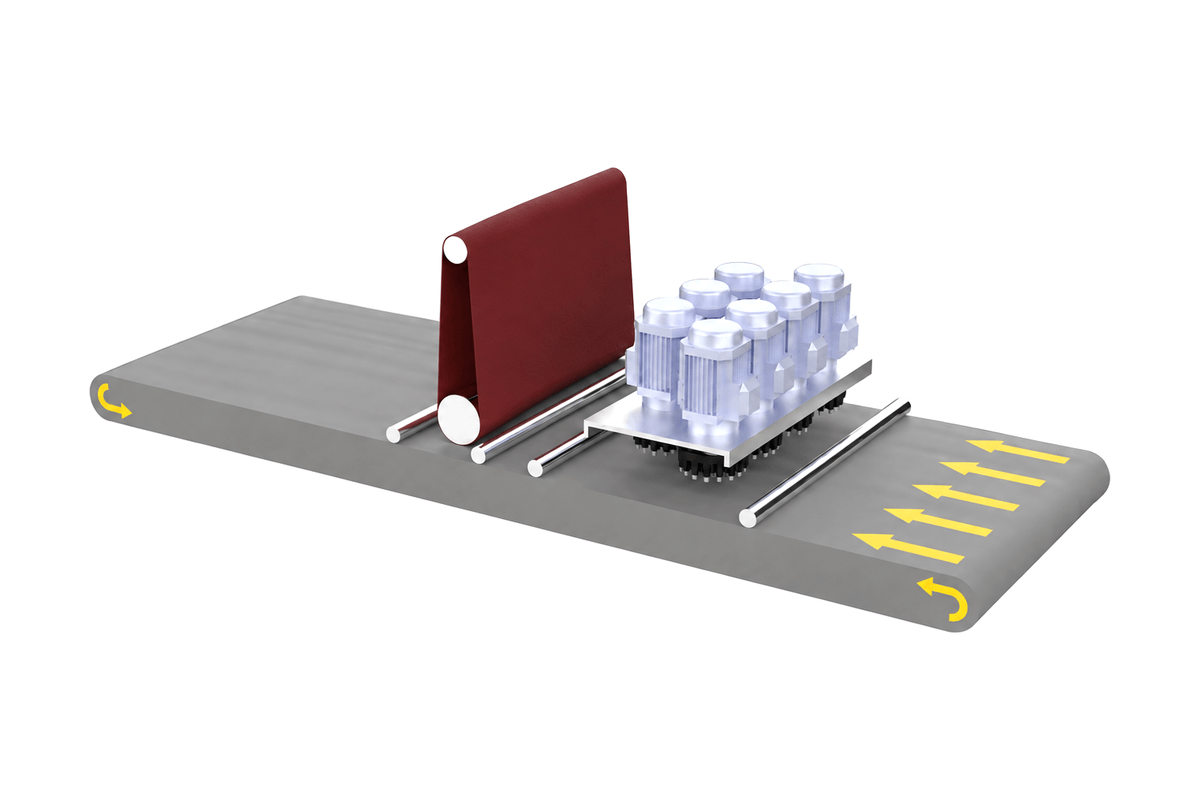
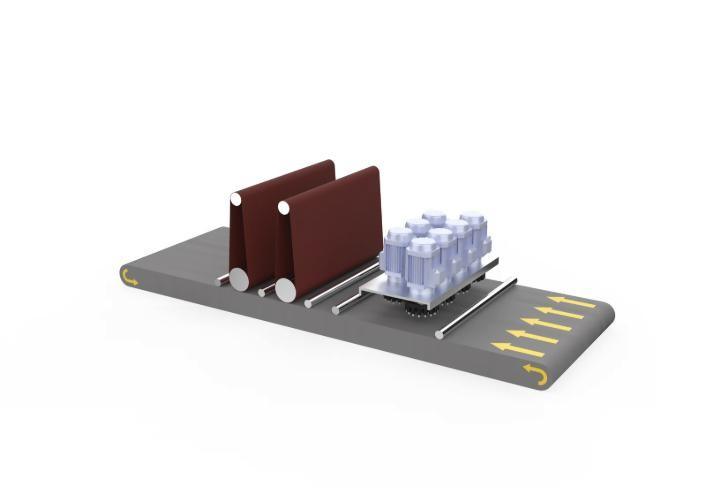
The hammer disc station does the work a chipping hammer does by hand. The discs strike the slag and fracture it off the edge before the belts clean what is left.
Need rounded edges after slag removal? A custom HBR configuration adds a rotary brush station after the hammer disc and belt.
Specifications
| Specification | Detail |
|---|---|
| Working widths | 800, 1000, 1300 and 1600 mm |
| Part thickness | 0.5 to 80 mm |
| Minimum part size | 15 x 15 mm on the magnetic table; 50 x 50 mm on the vacuum table (solid sheet) |
| Feed speed | 1 to 5 m/min, adjustable |
| Abrasive belt speed | 5 to 13 m/s |
| Compressed air | 0.5 to 0.8 MPa |
| Power supply | 415 V, 3-phase, 50 Hz |
| Control | Siemens PLC and touch screen, closed-loop servo drive |
| Part holding | Magnetic table for carbon steel; vacuum table for stainless, aluminium, copper and other non-magnetic parts |
| Safety | Interlocked doors, emergency stops, air pressure and over-thickness alarms |
| Materials | Carbon steel, stainless steel, galvanised steel, copper, aluminium (with wet dust collection) |
| Warranty | Two years, with installation, training and service from our Melbourne workshop |
Before and after
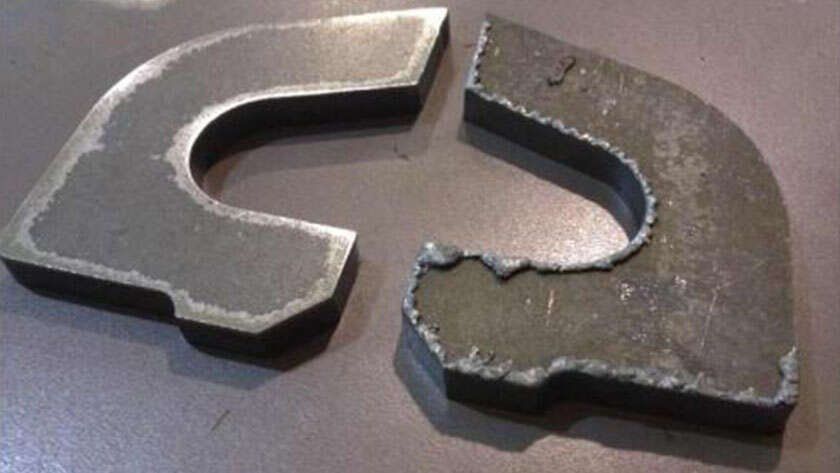
Processed part (left) beside an as-cut part with heavy slag (right).
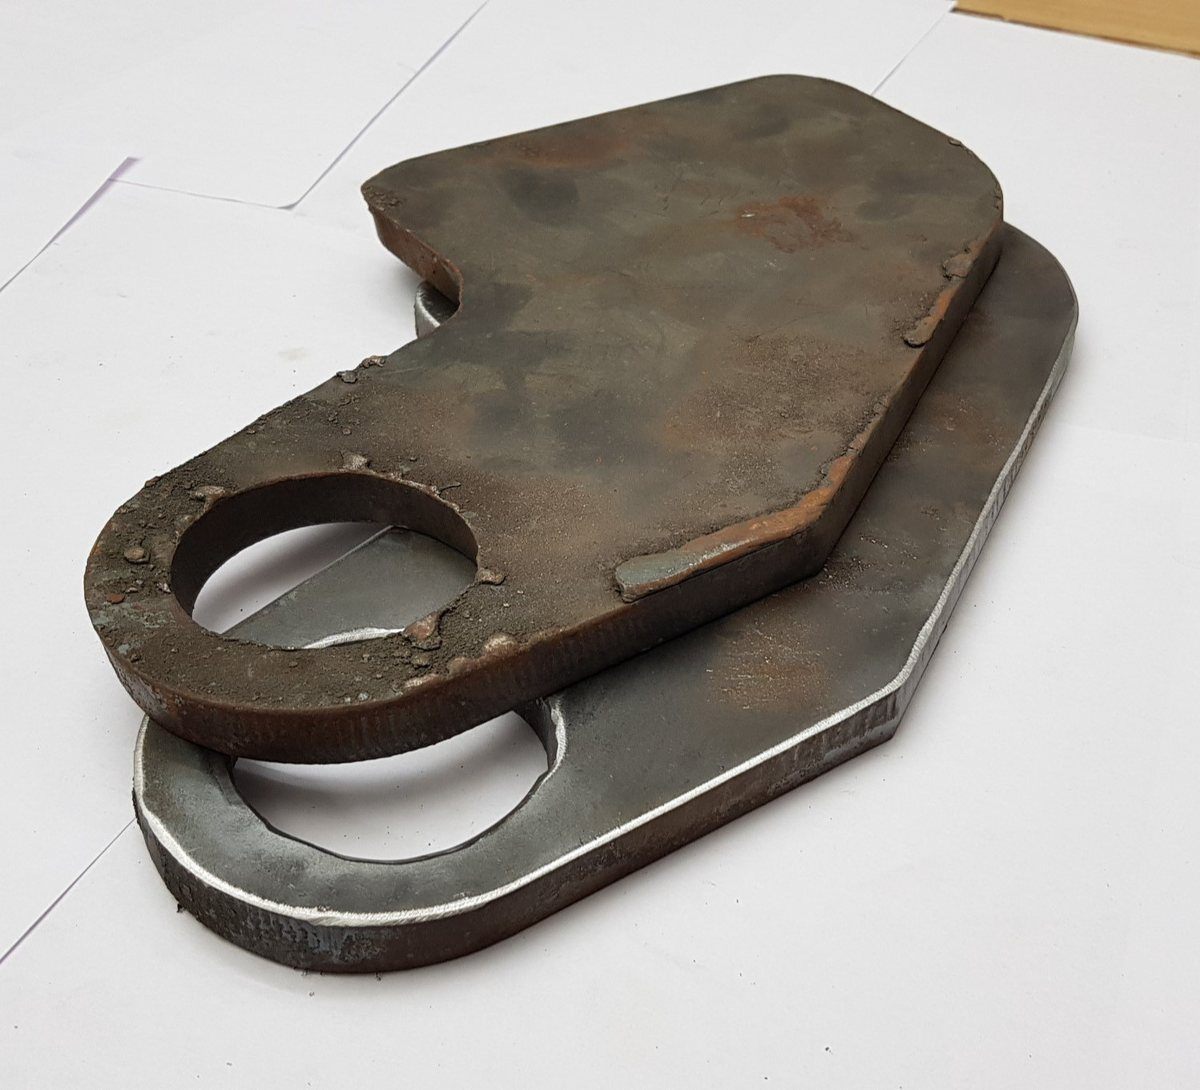
As-cut plate with slag and scale, on top of a processed plate.
Standard models
| Model | Stations | Size L x W x H (mm) | Weight (kg) | Installed power (kW) |
|---|---|---|---|---|
| 800HB | Hammer disc, belt | 2,820 x 1,847 x 2,200 | 1,850 | 22 / 37 |
| 1000HB | Hammer disc, belt | 2,820 x 1,850 x 2,200 | 2,150 | 25 / 40 |
| 800BB | Belt, belt | 2,130 x 1,500 x 2,200 | 1,700 | 17.5 / 32.5 |
| 1000BB | Belt, belt | 2,480 x 1,830 x 2,250 | 2,300 | 24.5 / 39.5 |
Is it the cut or the clean-up?
Heavy dross on laser-cut plate is not always a finishing problem. A worn nozzle, a contaminated protective window, the wrong focus position or low assist gas pressure will all leave slag that a healthy machine would not. We service laser cutting machines every day, so we check the cut before we sell you a machine to clean up after it.
Where it fits
- Plasma-cut and oxy-cut carbon steel plate
- Thick plate from high-power fibre lasers
- Structural steel components
- Weld preparation
- Powder coat and paint preparation
Questions we get asked
What is the difference between dross and slag?
Both are metal that melted during cutting and re-solidified on the bottom edge. Light dross from a laser usually comes off with an abrasive belt. Heavy slag from plasma, oxy-fuel or thick-plate laser cutting is harder and more firmly attached, and needs the hammer disc station.
Will it remove slag from the whole part or just the edge?
The hammer discs and belts work across the full working width, so the whole face of the part is processed as it feeds through.
Do I still need to grind by hand afterwards?
For most flat plate, no. We confirm it on your own parts before you commit.
What thickness of plate can it handle?
From 0.5 mm up to 80 mm.
Can it handle aluminium?
Yes, with a wet dust collector specified for the job.
Send us your worst plate.
Pick the parts your team least wants to grind. We will show you what they look like after one pass.
Call 03 9796 3055 or email sales@industriallaser.com.au